Est. 2009 · Meerut, India
A sports equipment factory built around export.
VEXORA Sports manufactures across ten sports categories and ships to thirty-four markets. We are a factory with an export desk attached — not a trading house with a factory attached.
Our story
Sixteen years, one discipline.
VEXORA began in 2009 as a cricket and team-ball workshop in Meerut — a city that has made sports goods for more than a century. The first export order, to a UK club distributor in 2013, changed how we worked: a buyer eight thousand kilometres away cannot inspect a line, so everything had to be written down, sampled and audited instead.
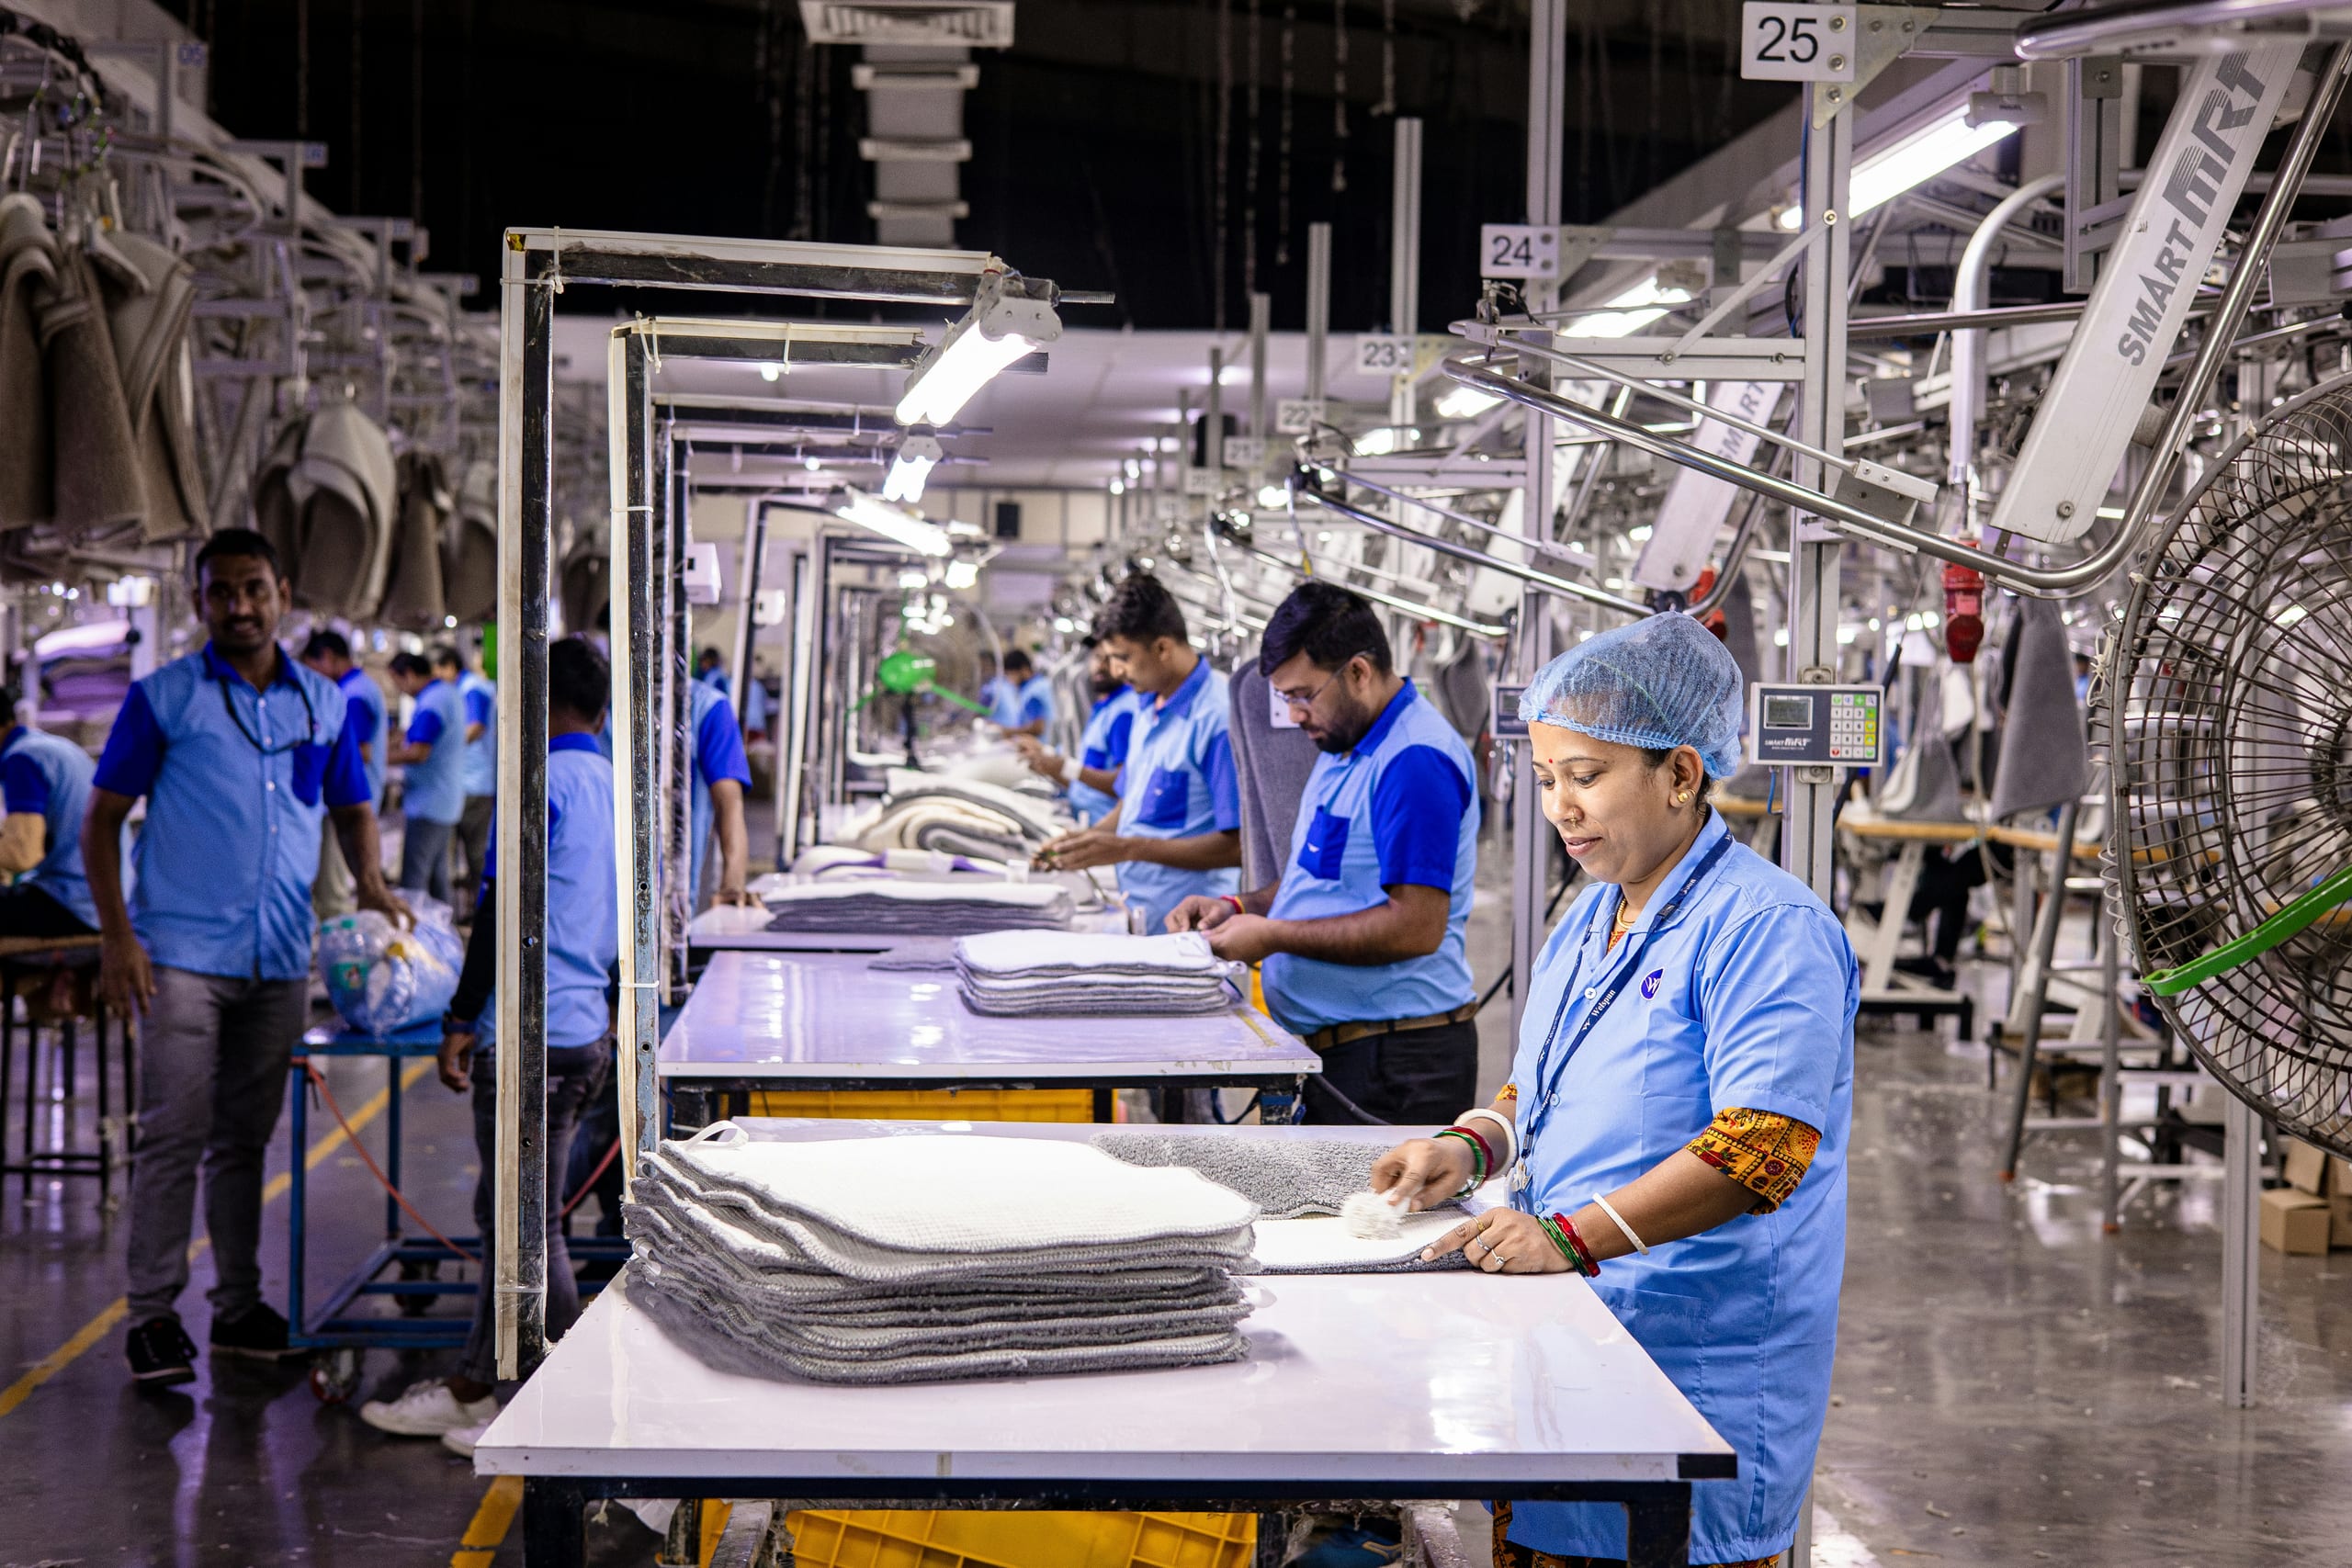
That constraint became the business. Today 420 people work across 118,000 sq ft of manufacturing floor, producing roughly 2.4M units a year. We still make cricket bats. We also mould basketballs, sublimate jerseys, press shin guards and build wheeled kit bags — all under the same roof, to the same written standard.
Most of what leaves our gate carries somebody else's brand on it. That suits us. Our name is on the specification sheet and the inspection report, which is where it matters.
Milestones
How the factory grew.
Each step was a response to what export buyers actually asked for — more categories, tighter tolerances, faster sampling.
2009
Founded in Meerut
Started as a cricket and team-ball manufacturer serving the domestic Indian market.
2013
First export contract
Began supplying UK and UAE distributors; export desk established as a separate function.
2016
Factory expansion
Moved to the current 118,000 sq ft facility, adding moulding and sublimation lines.
2019
OEM division launched
Dedicated development team formed to run private-label and bespoke tooling programmes.
2022
Quality system formalised
Three-stage inspection protocol and AQL sampling adopted across every product line.
2025
34 markets
Exporting across six continents with in-house documentation and freight coordination.
How we work
Three commitments, kept narrow on purpose.
We would rather do a small number of things dependably than claim a long list we cannot evidence.
01
Specify it, then build it
Every order starts with a written specification and a signed golden sample. Ambiguity is where import disputes come from, so we remove it before the first unit is cut.
02
Own the process
Moulding, pressing, stitching, sublimation and finishing are all ours. When something needs changing we change it, rather than asking a subcontractor to.
03
Tell the truth about dates
We quote lead times we can hold and flag slippage the day we see it. A realistic date you can plan around beats an optimistic one you cannot.
One supplier, ten categories
Consolidate a mixed catalogue onto a single purchase order, a single container and a single set of export documents.
Specification you can audit
Every product ships against a written specification and a signed golden sample — so what arrives is what you approved.
Tooling that stays yours
Moulds and patterns developed for your OEM programme remain your property and are never run for another buyer.
Export desk, not a sales desk
Documentation, inspection coordination and freight booking handled in-house. One contact from enquiry through to delivery.
Manufacturing
Capability you can walk through.
Moulding, pressing, cutting, stitching, sublimation and finishing all sit under one roof. Nothing critical is subcontracted, which is why our lead times hold.
26
Production lines
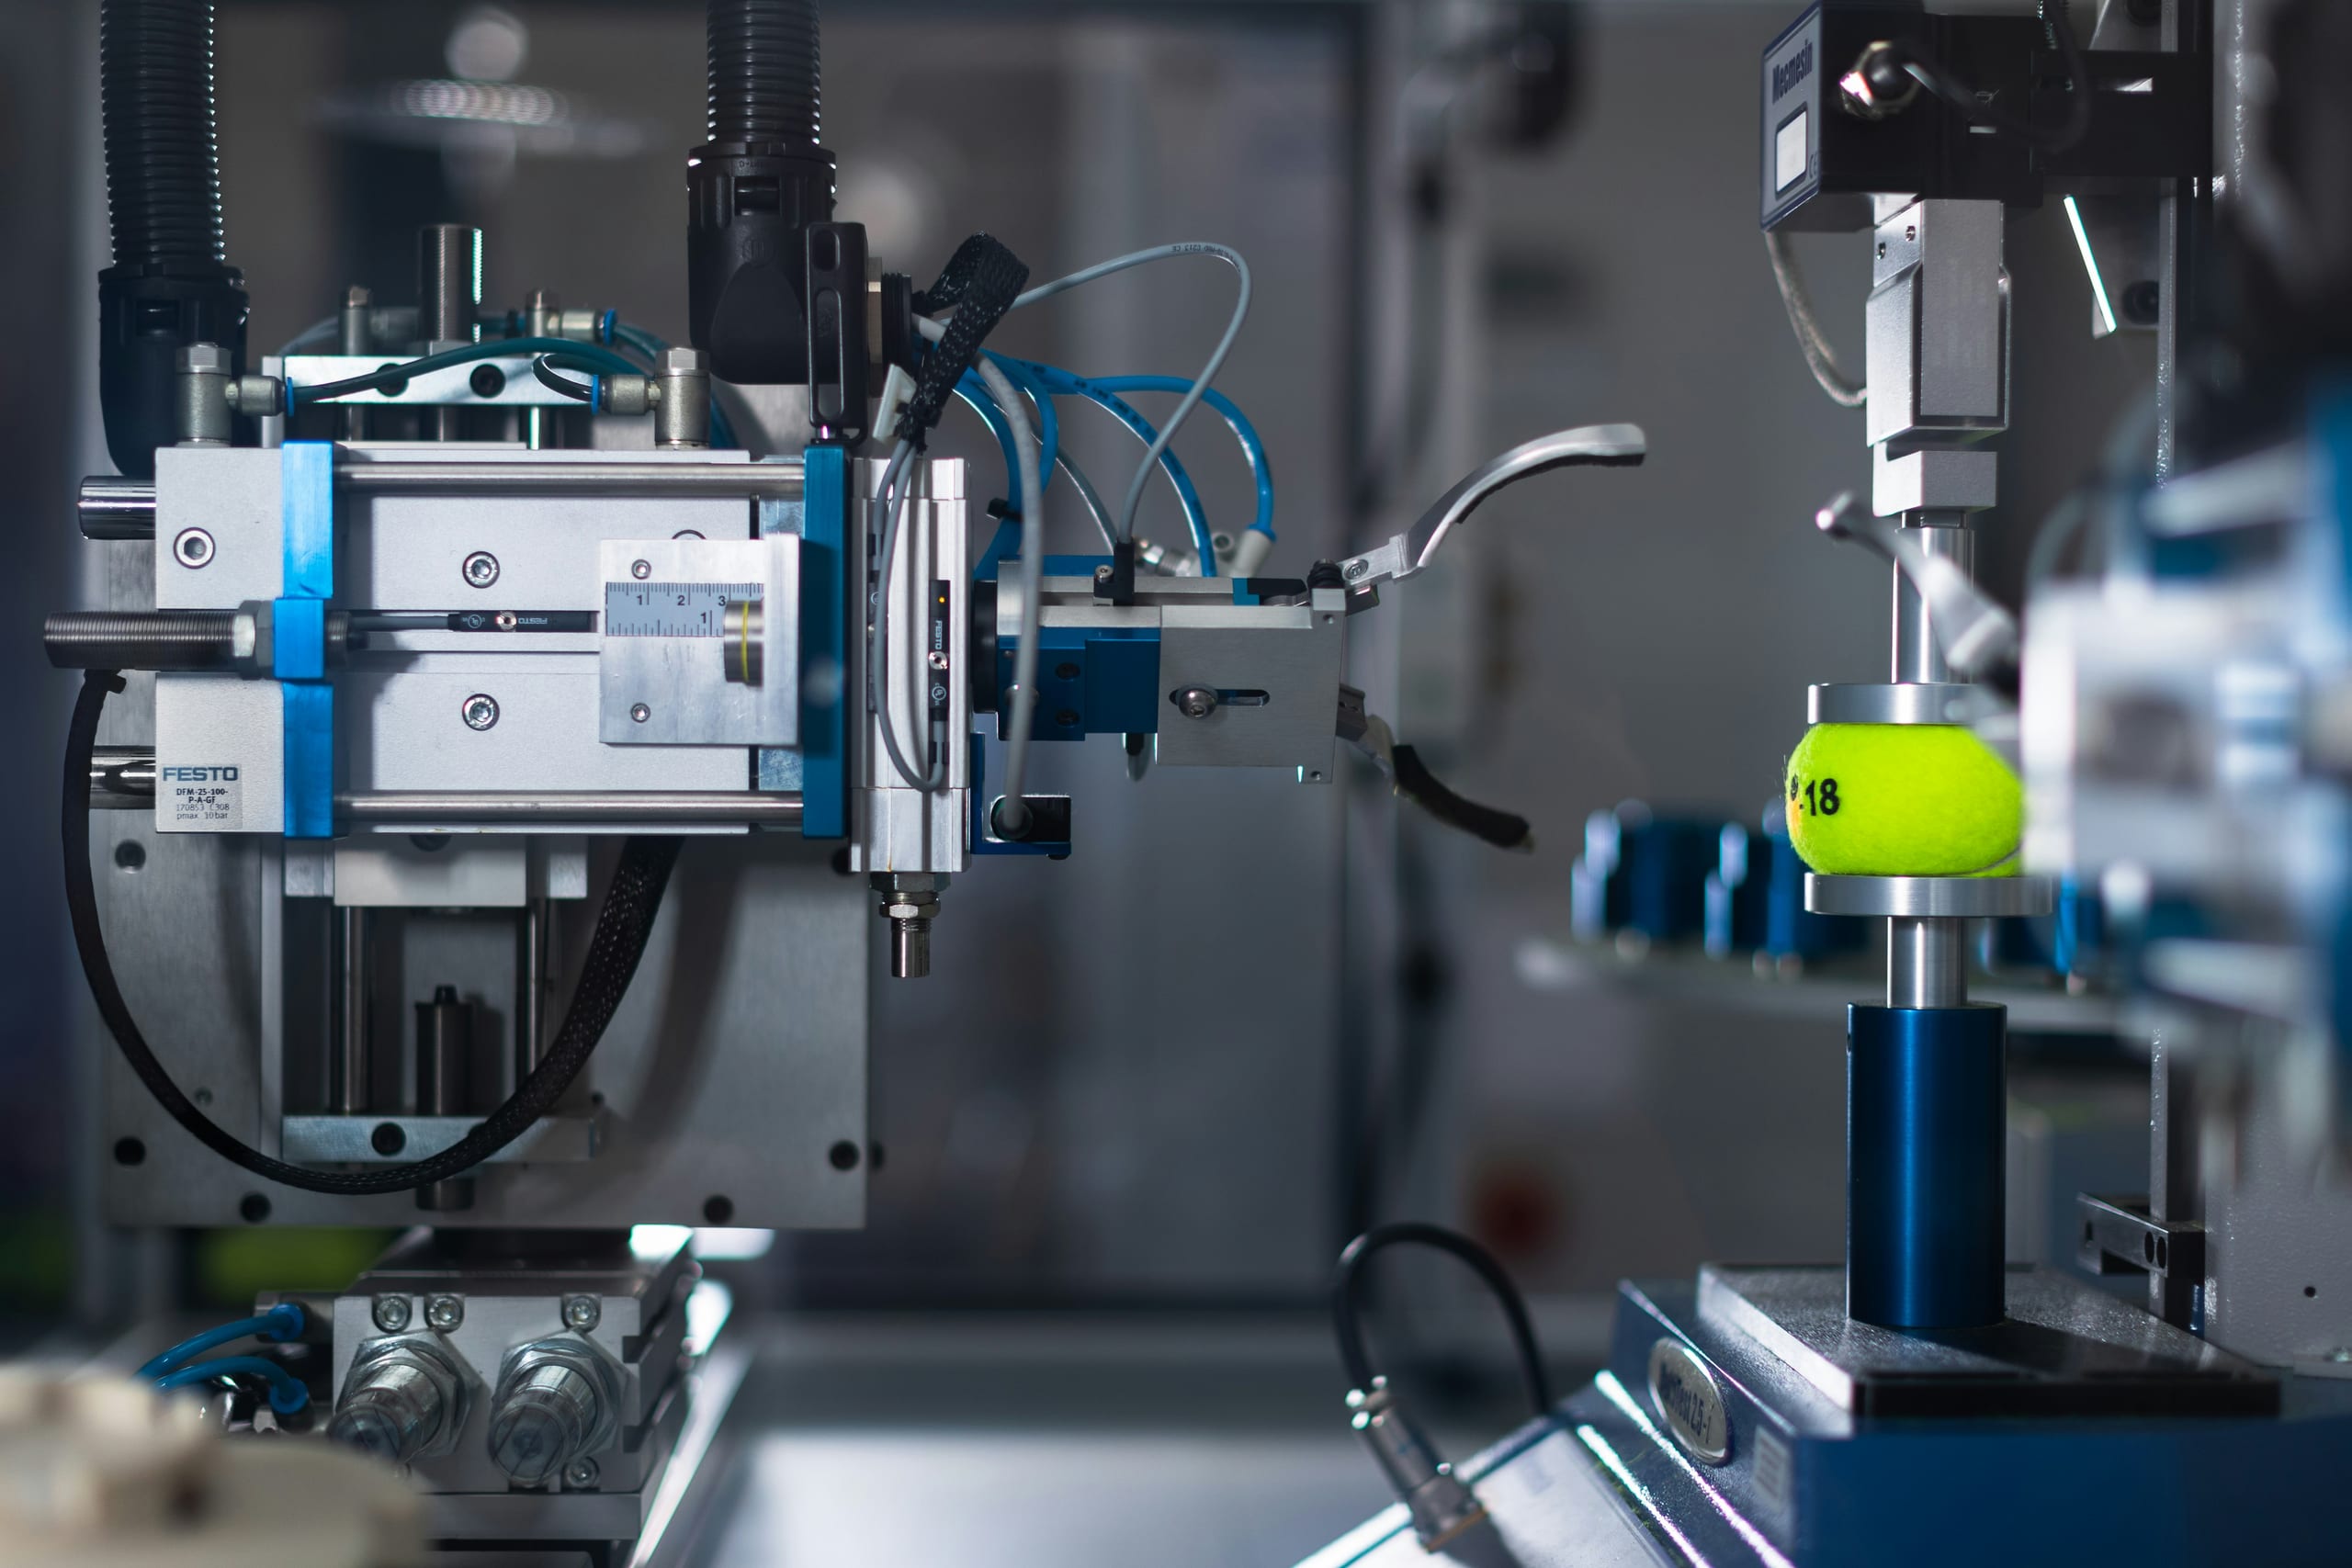
In-house moulding & pressing
Compression and injection moulding for balls, guards and grips, plus a dedicated willow pressing shop. Running the tooling ourselves is what keeps a repeat order inside the tolerance you approved on the first one.
180
Stitching stations
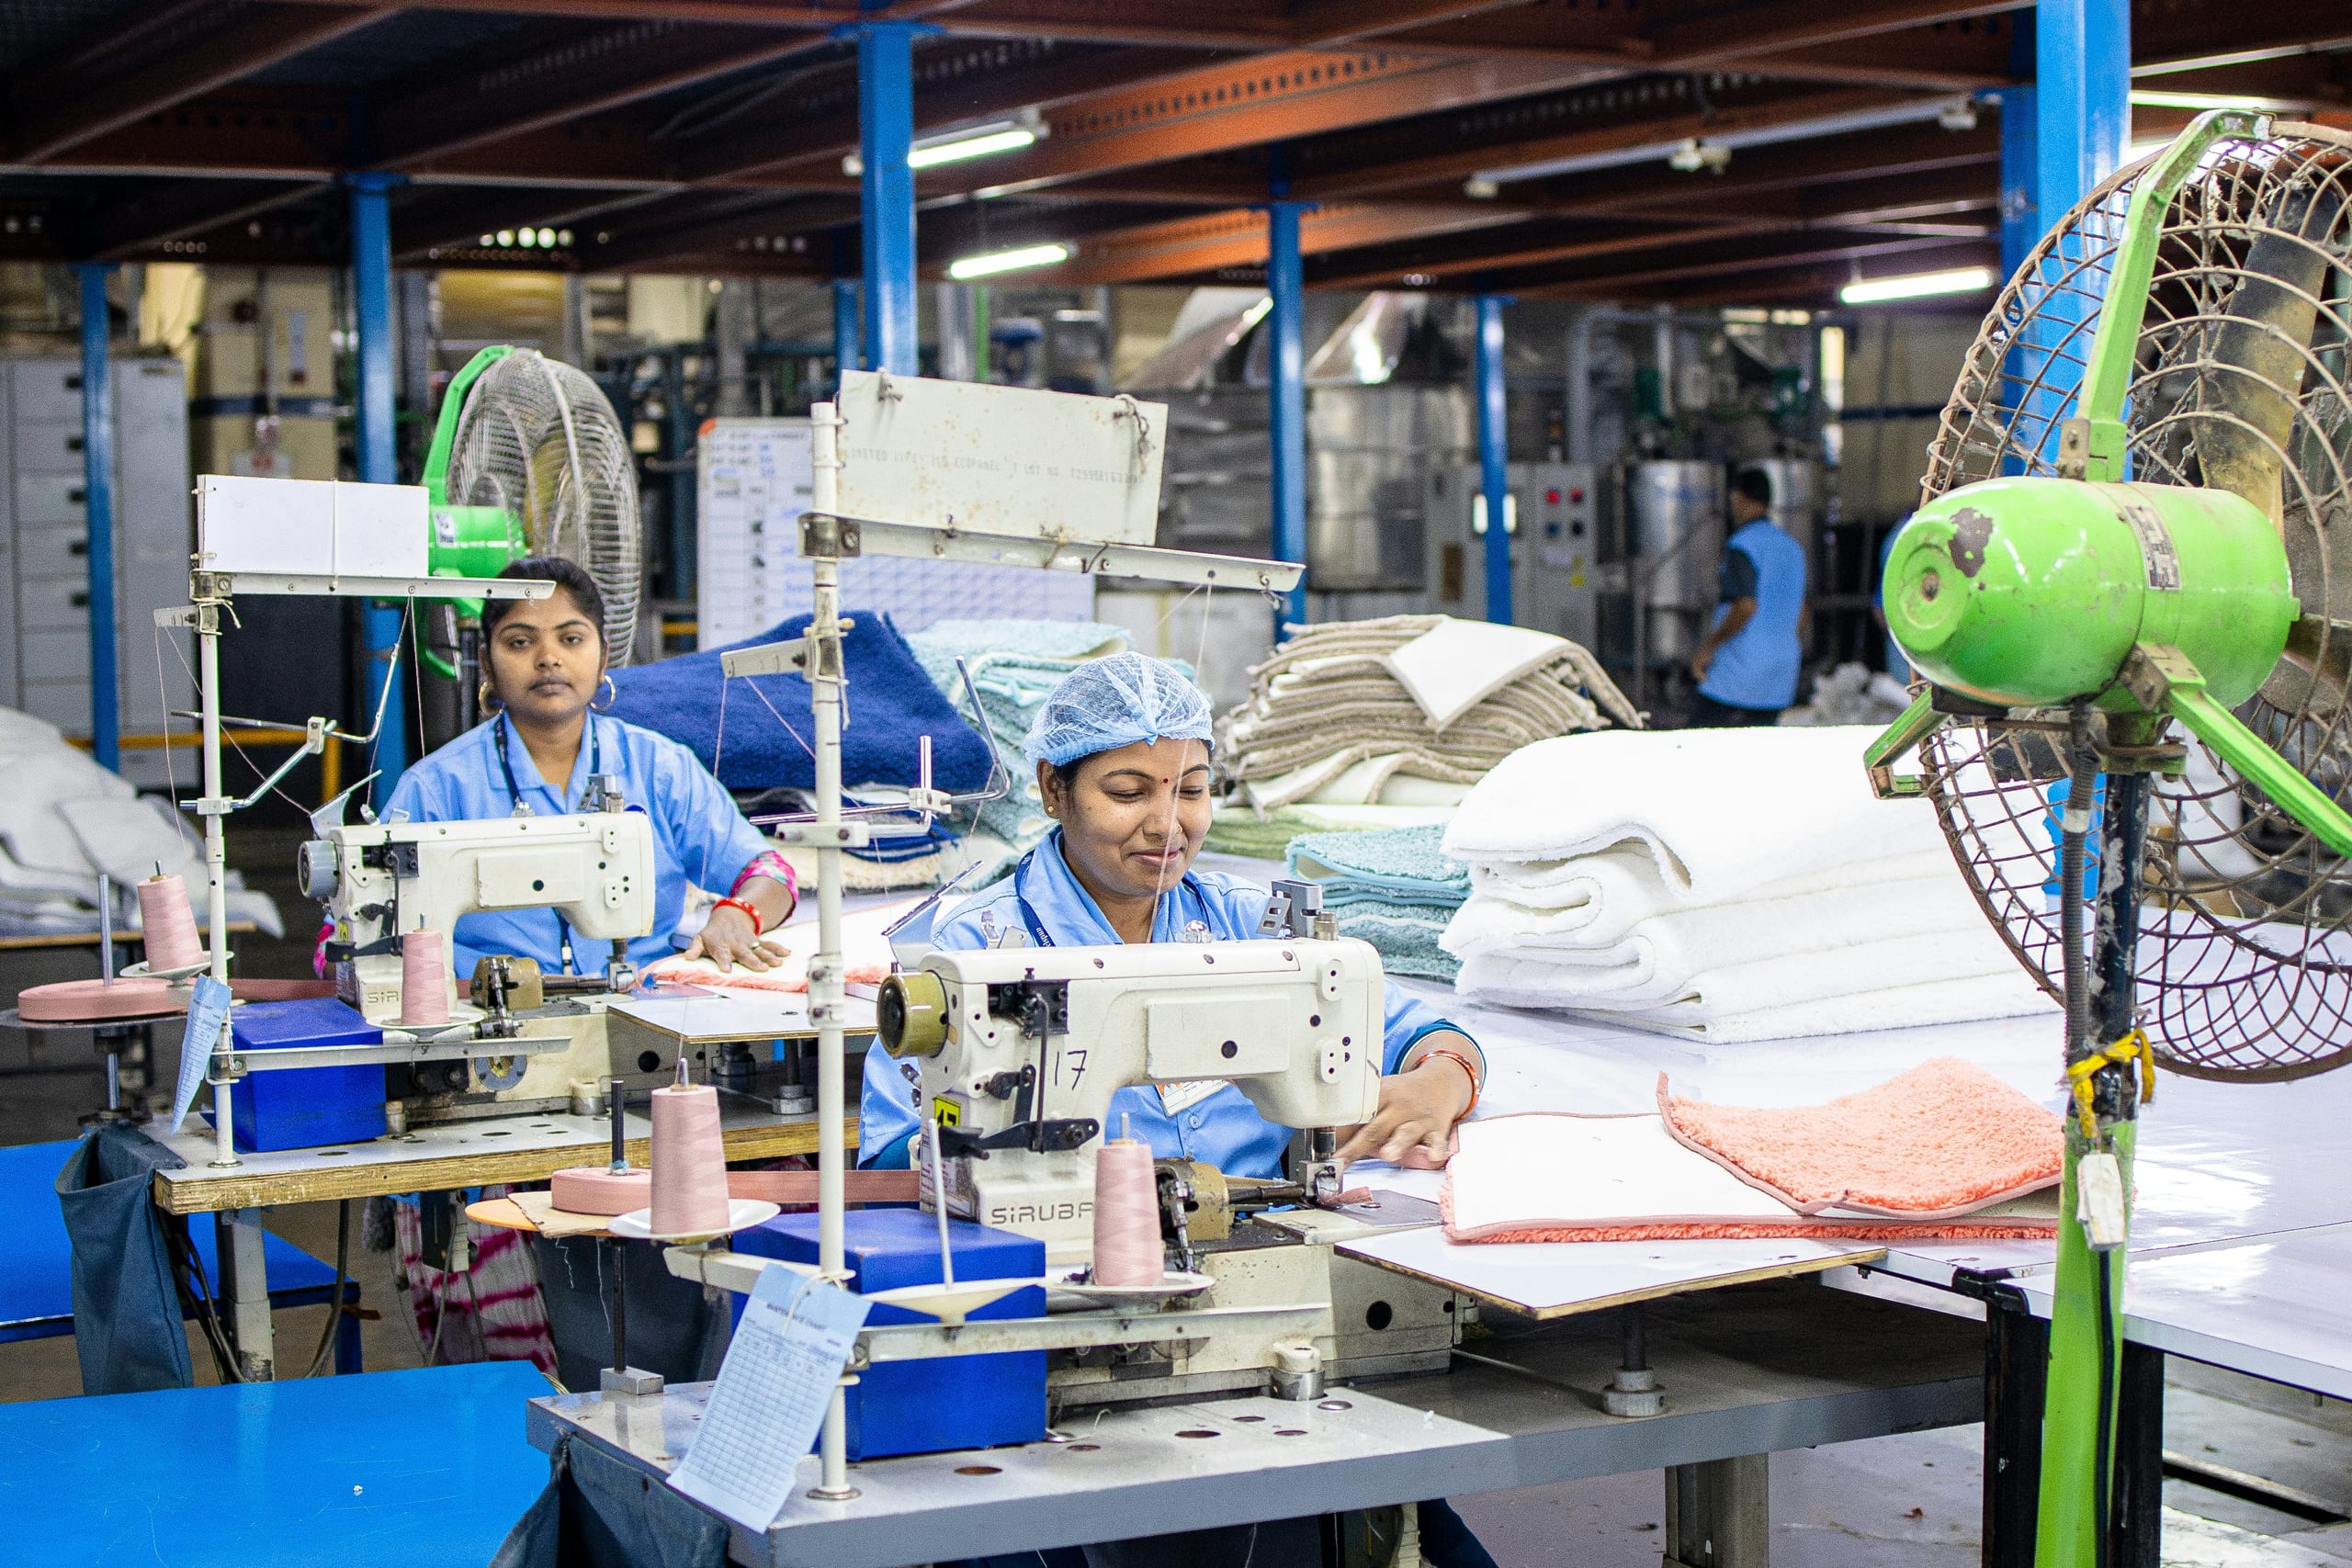
Cutting, stitching & assembly
Automated cutting tables feed 180 stitching stations across leather, PU and technical textile lines. Hand-stitching cells are retained for match-grade balls where machine stitch cannot match seam integrity.
100%
Incoming lots tested
Material sourcing & testing
Leather, latex, EVA and polyester are bought against a written specification and tested on arrival for thickness, tensile strength and colour fastness. Rejected lots never reach the floor.
160k
Garments / month
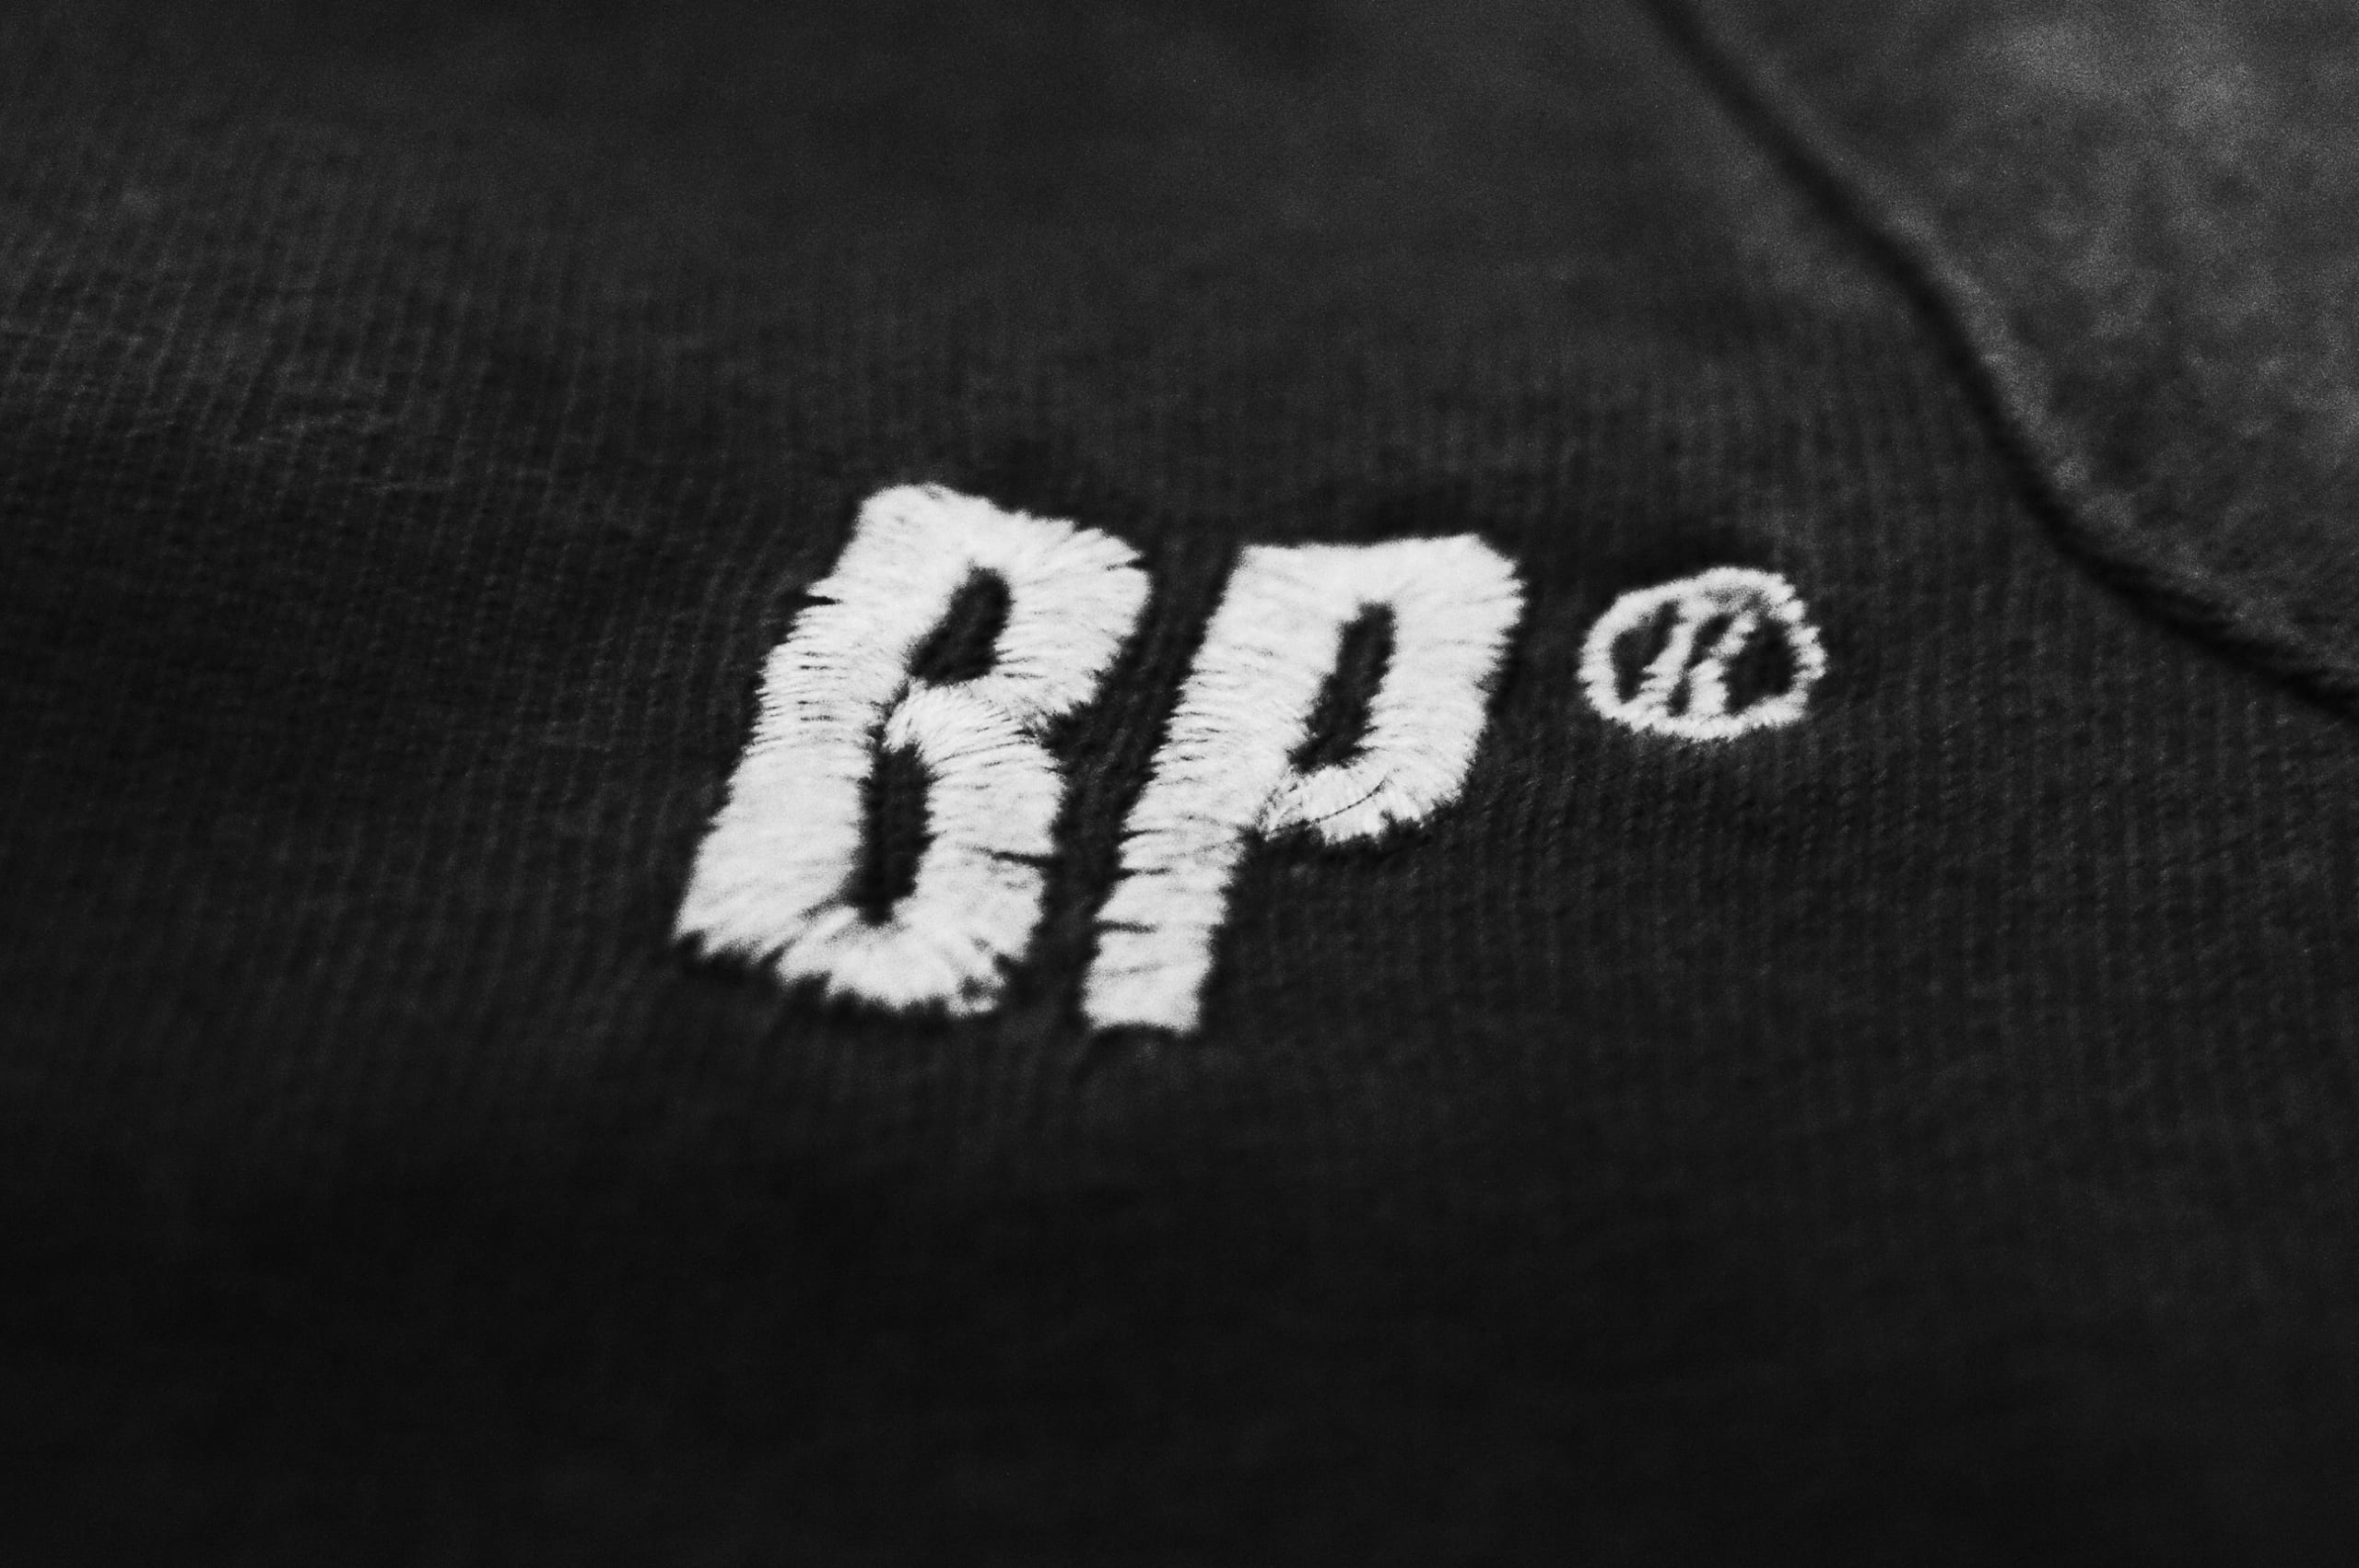
Sublimation & finishing
Two sublimation lines and an embroidery bank handle garment, bag and glove decoration in-house, so branding is never subcontracted and artwork approval is a single conversation.
Request a quote
Work with the factory directly.
No agents, no layers. Send your specification and you'll be talking to the people who run the line.
- Response time
- < 1 working day
- Sample lead time
- 12–18 days
- Incoterms
- EXW / FOB / CIF / DDP